
The Core Challenge in Thin-Wall Food Packaging Molding
Food packaging producers working with thin-wall containers — yogurt cups, drink cups, meal boxes, and disposable food containers — face a specific set of operational pressures: melt must fill an extremely thin cavity before it solidifies, multi-cavity molds must hold dimensional consistency across every cycle, and any slowdown in cycle time directly erodes unit economics. According to published process guidance in this field, thin-wall molding is generally defined as wall thickness between 0.2mm and 0.6mm for a molding area under 0.1m², with larger-area parts qualifying up to 1.5mm. For a 0.4mm wall thickness, filling time is typically only 0.2 to 0.3 seconds — a window that leaves no room for sluggish injection systems, uneven venting, or imprecise mold steel selection.
DKM Machinery and SINO MOULD, operating as a joint technology provider covering injection molding machines, precision molds, robotics, and complete one-stop turnkey plastic injection molding production lines, have built their thin-wall capability specifically around this problem. The two companies describe 15 years of thin-wall injection molding research, with over 600 sets of thin-wall machines and molds produced per year, and have tested their DKM-HH and DKM-DFS series at injection speeds of 300-500 mm/s to validate performance against the demands of high-speed thin-wall production.
High-Speed Machine Platforms Built for Thin-Wall Output
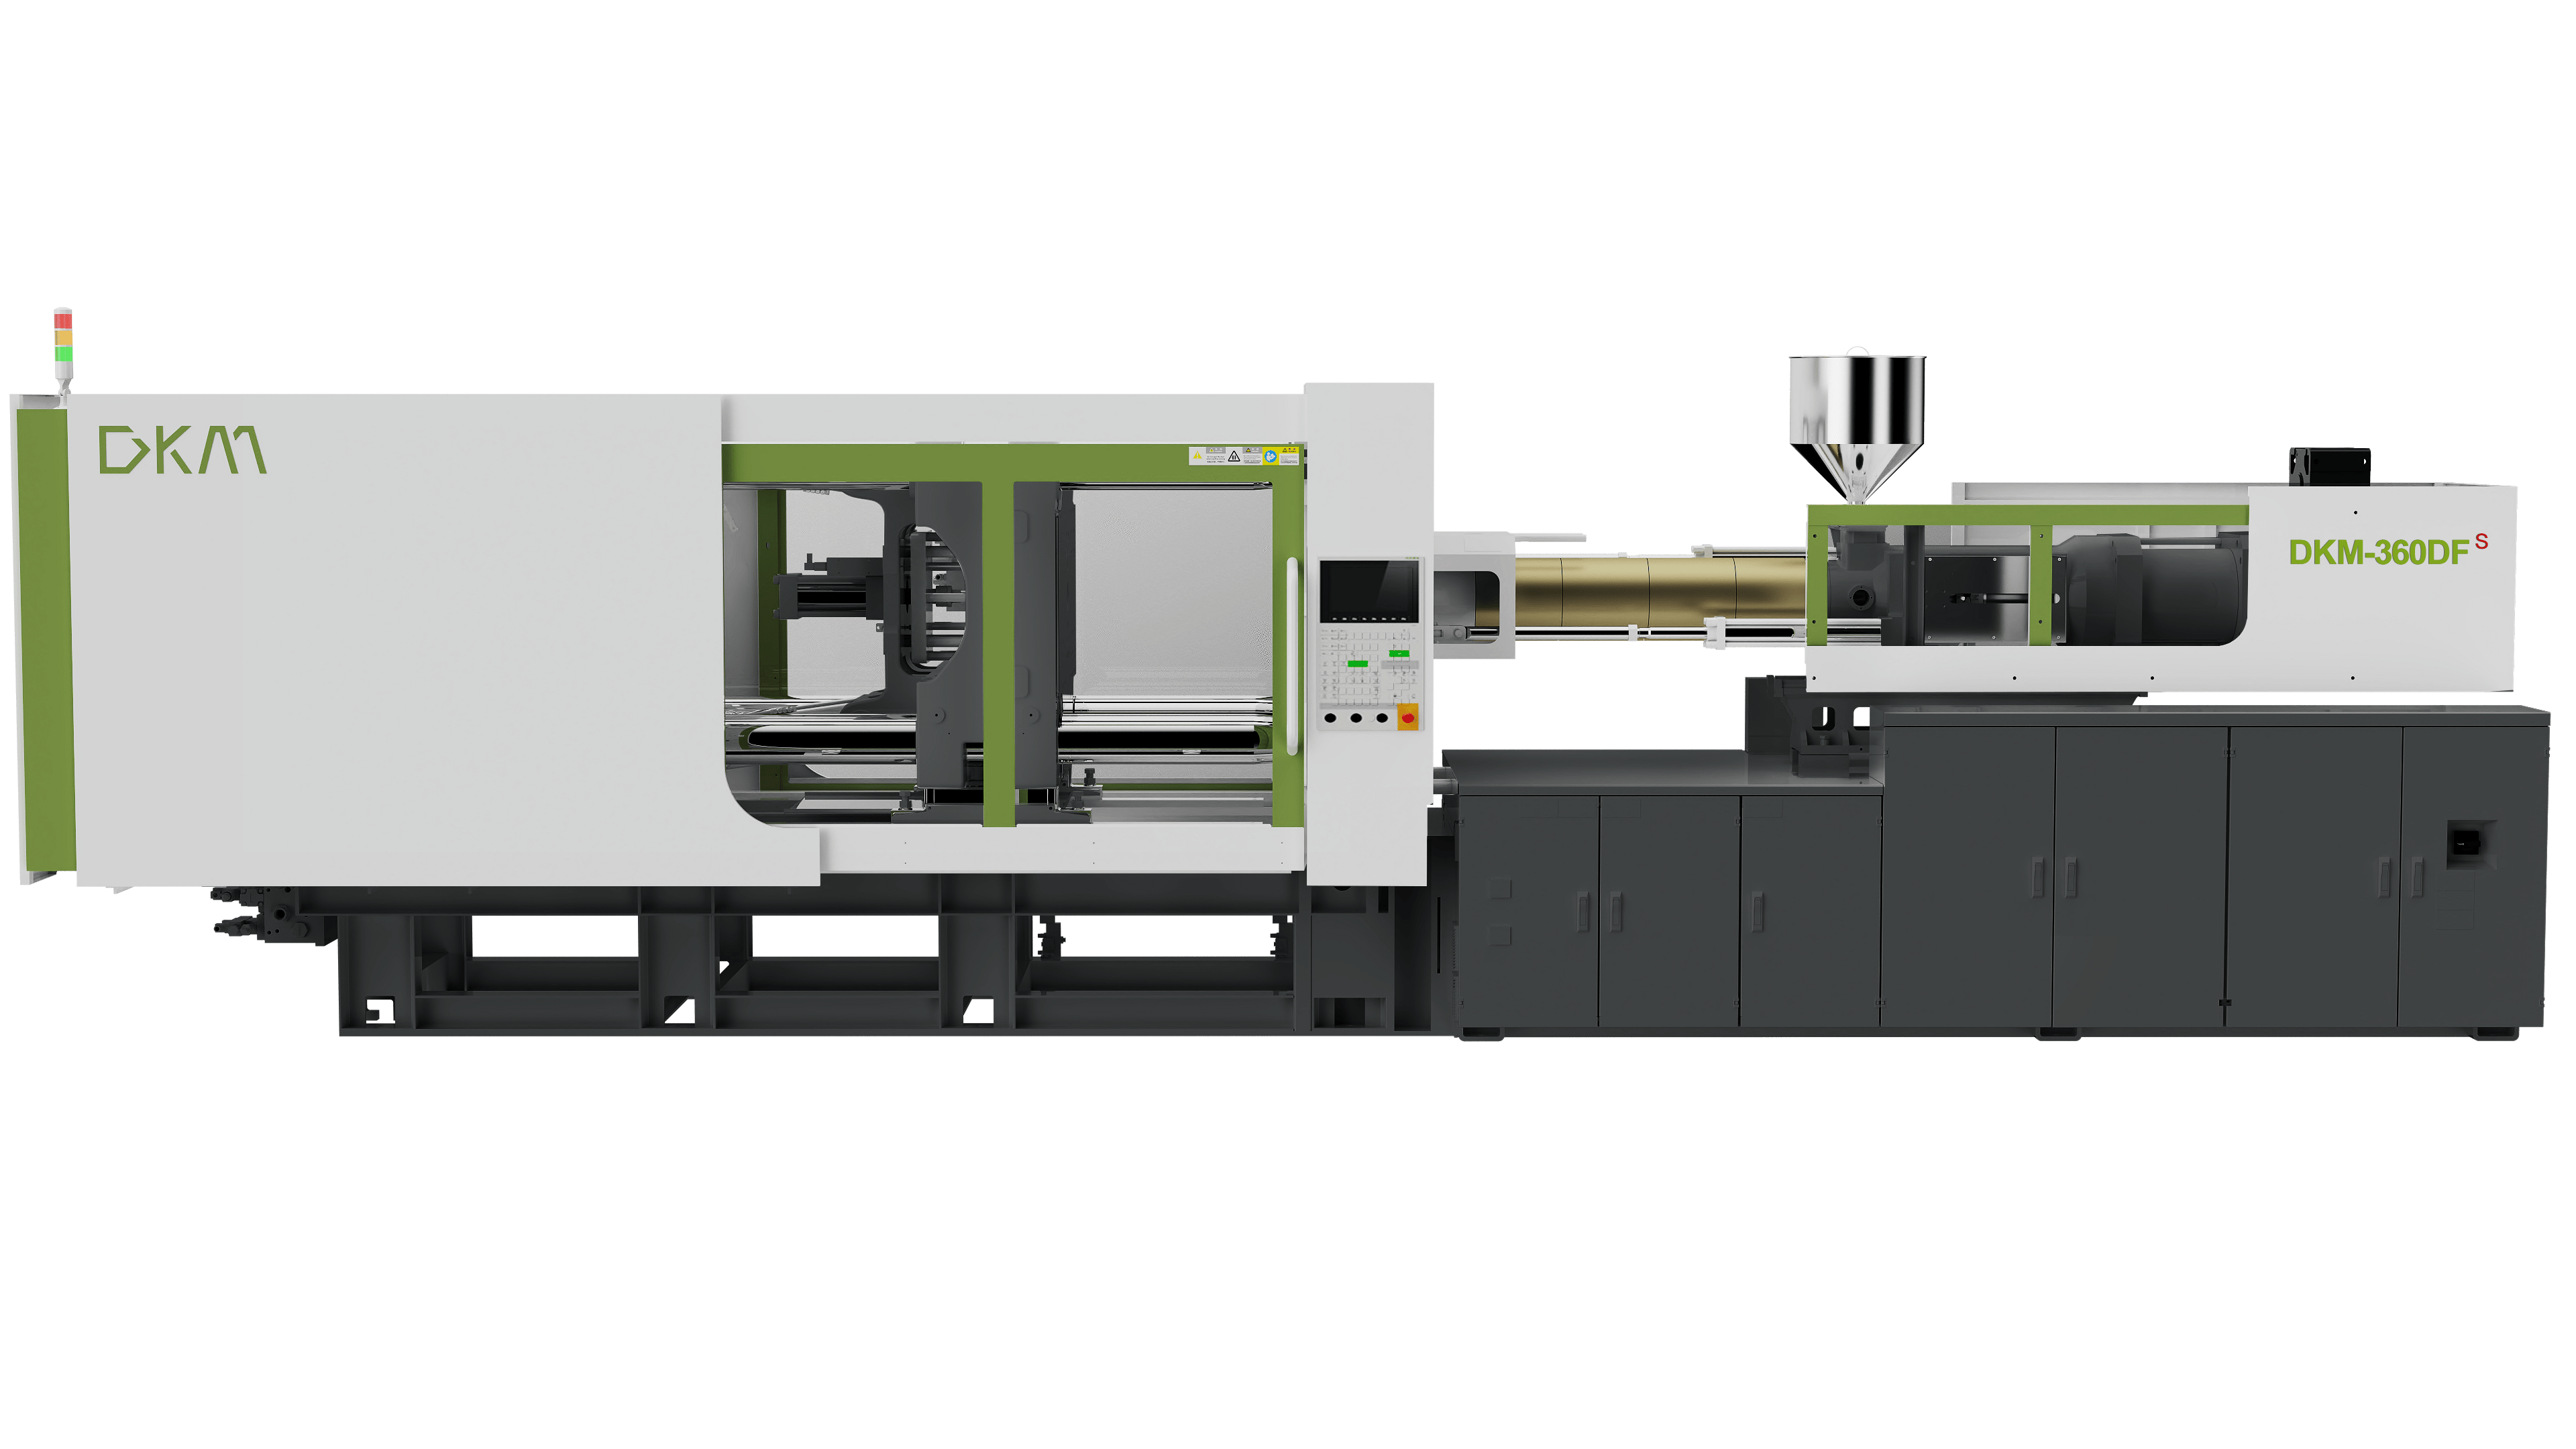
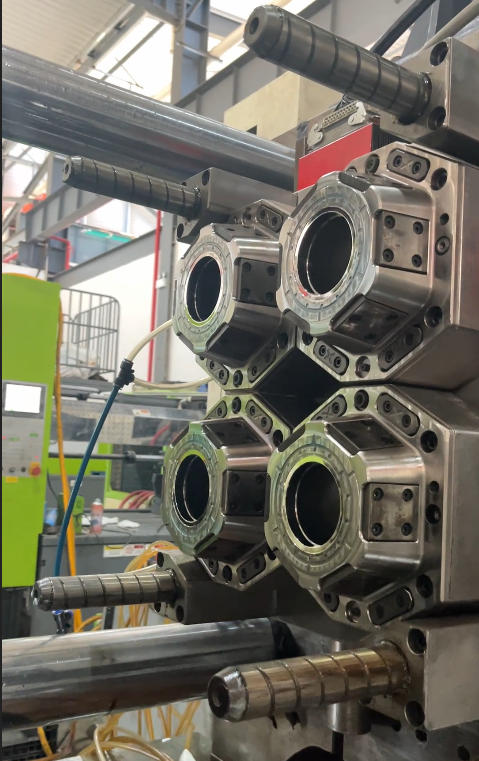
Two machine series anchor the thin-wall offering. The DFS Series Fast Speed Injection Molding Machine is a hybrid toggle platform available in 250T, 310T, 360T, and 460T clamping forces, purpose-built for thin-wall applications. It reaches an injection speed of 444 mm/s in 0.13 seconds, with a maximum injection speed of 500 mm/s, and uses patented low-inertia injection technology that reduces moving unit weight to approximately half that of standard machines. Electric charging allows mold opening, ejecting, and pre-charging to run simultaneously, shortening cycle time by 30-50% versus conventional thin-wall lines. A single-cylinder injection system delivers stable, consistent injection pressure, and shot weight tolerance is held to ≤2‰. The design also removes the nitrogen accumulator in favor of a larger oil pump motor with a 40% power boost, reducing maintenance needs while cutting energy consumption by 25-30%. More than 200 DFS units are reported running across China with validated field performance.
The HH Series High Speed Plastic Injection Molding Machine complements this range from 200 to 1300 tons, reaching injection speeds of 300-500 mm/s to meet thin-wall filling requirements while supporting high productivity and flexibility. An internal heating design concentrates heat between the barrel and screw, keeping external temperature below 50°C and reducing thermal energy waste — a feature consistent across both the HH and DFS lines.
On the all-electric side, machine requirements for thin-wall work are defined as 200-800 mm/s injection speed, high-precision injection, rapid mold opening and closing, and 3-axis linkage — specifications these machine platforms are engineered against.
Mold Precision That Matches Machine Speed
A fast machine alone cannot solve thin-wall molding; the mold must keep pace. SINO MOULD's Thin-Wall Mold line is built on DIN 1.2344 steel, selected over S136 for high-temperature, high-speed, high-pressure molding, since S136 offers only rust prevention with lower high-temperature performance, strength, and wear resistance. Molds feature 100% uniform air venting to support instantaneous filling of roughly 0.3 seconds, synchronized valve gate opening for multi-cavity consistency, and balanced core/cavity thermal expansion to prevent self-locking misalignment. Core/cavity temperature difference is controlled within ≤±1°C, and mold component tolerance is held to 0.01mm. In high-heat zones, beryllium copper — with 5-8 times the thermal conductivity of H13 — is combined with cooling steel for strength and wear resistance. Thin-wall and IML molds carry a qualified delivery window of within one month.
Integrated IML Lines: Labeling Without Slowing Down
For food packaging that requires in-mold labeling, DKM, SINO MOULD, and IVI ROBOT jointly deliver a complete Thin-Wall IML Production Line that integrates the DFS injection machine, an IML mold suitable for 0.28-0.4mm wall thickness, an in-mold labeling robot, and precision temperature control. The line achieves a molding cycle of 2.8-3.5 seconds — stated as over a 50% improvement versus traditional lines — while maintaining ultrathin walls from 0.28mm, high gloss, consistent dimensions, and a yield rate of ≥99%. Moog servo valves paired with a KEBA controller deliver 1‰ repeatability, and the IVI ROBOT in-mold labeling robot achieves label positioning accuracy of ≤0.01mm, with a fully synchronized pick-label, insert, mold, and part-removal workflow that allows plasticizing, ejection, labeling, and removal to run in parallel for unmanned production.
This architecture has produced measurable results in food packaging applications. On a 500-1000ml PP/PS tea or drink cup, a DKM-360DFS machine running an 8-cavity thin-wall IML mold achieves a 6-second cycle. On a yogurt cup application, a DKM-310DFS machine with a 4-cavity IML mold achieves a 5.3-second to 5.8-second cycle. At CHINAPLAS 2025, an 8-Cavity Thin-Wall IML Intelligent Cup Production Line combining the DKM-360DFS with a high-speed IVI-IML robot was demonstrated producing an 8-cavity, 0.35mm-thick cup with a 120mm cavity height at a 5.5-second cycle time.
Platform and Delivery Backing
This thin-wall capability sits inside a broader technology platform that includes a European R&D team organized by an Italian two-platen machine specialist with 25+ years of experience, a Technical Office in Italy established in 2018, and a Technology Center in Italy established in 2023. Over the past ten years, R&D expenditure has accounted for 8%-10% of sales revenue. DKM Machinery and SINO MOULD operate across more than 100 countries and regions, with business covering packaging, home appliance molding, medical consumables, and logistics industries.
For food packaging producers evaluating a high-speed thin-wall container line, the combination of a DFS or HH series machine, a DIN 1.2344 thin-wall mold engineered for ≤±1°C core/cavity balance, and an IVI ROBOT-integrated IML workflow offers a documented path to the cycle-time and yield outcomes described above. Thin-wall and IML molds are available with qualified delivery within one month, and the companies state a professional engineering response within 24 hours for technical support throughout commissioning and production ramp-up.
https://dkm.com/dfs-low-inertia-high-speed-machine/
DKM Machinery

+ There are no comments
Add yours