
Why Oil Bottle Preform Line Investment Decisions Hinge on Mold and Machine Integration
For producers packaging edible oil and other liquid products in PET bottles, the preform stage is where output volume, material cost, and bottle quality are largely determined. A preform production line must deliver consistent cavity-to-cavity weight, dimensional accuracy at the neck finish, and fast cycle times without sacrificing mold life. These are the same engineering requirements that govern water and beverage preform manufacturing, and they are the foundation of the PET Preform Production Line developed jointly by DKM Machinery and Sino Mould, two entities operating under the DKM Machinery / Sino Mould Co., Ltd. group headquartered in Zhejiang, China, with business coverage across 100+ countries and regions.
The Core Engineering Problem in Preform Molding
Injection molding producers commonly face long equipment lead times, high per-unit production costs, slow molding cycles, and unstable multi-cavity consistency — pain points that apply directly to any bottle producer sourcing PET preforms, including those supplying oil packaging. A preform mold with 48, 72, or 144 cavities must hold tight tolerances across every cavity simultaneously; any deviation shows up as uneven wall thickness or inconsistent neck sealing once the preform is blown into a finished bottle. Addressing this requires combining a dedicated injection molding machine with a precision mold and an automated take-out system — rather than sourcing each component separately and attempting integration after delivery.
Machine and Mold Engineered as One System
DKM's PET Preform Production Line integrates the preform mold, the DKM-PET III preform-dedicated injection molding machine, and a take-out robot into a single pre-commissioned package. Three standard configurations illustrate how this system scales:
- Standard 1: PET 650 machine, 144 cavities, take-out robot, producing an 11g/29mm preform on a 12.8-second cycle
- Standard 2: PET 450 machine, 72 cavities, dual-station external cooling robot, producing a 12g/28mm preform on a 12-second cycle
- Standard 3: PET 350 machine, 48 cavities, three-station external cooling robot, producing a 12g/28mm preform on a 16-second cycle
The DKM-PET III series itself — spanning the DKM-350, DKM-450, DKM-550, and DKM-650 PET III models — is built around a standard electric accumulator for synchronized plasticizing combined with post-mold cooling technology, nano far-infrared heating rings for energy savings, and an optimized machine frame structure that achieves an injection repeat accuracy of ≤0.5‰. For any oil bottle preform program where multi-cavity consistency determines yield, this repeatability figure is a direct indicator of how uniformly each cavity will perform across a full production run.
Mold Precision Behind the Numbers
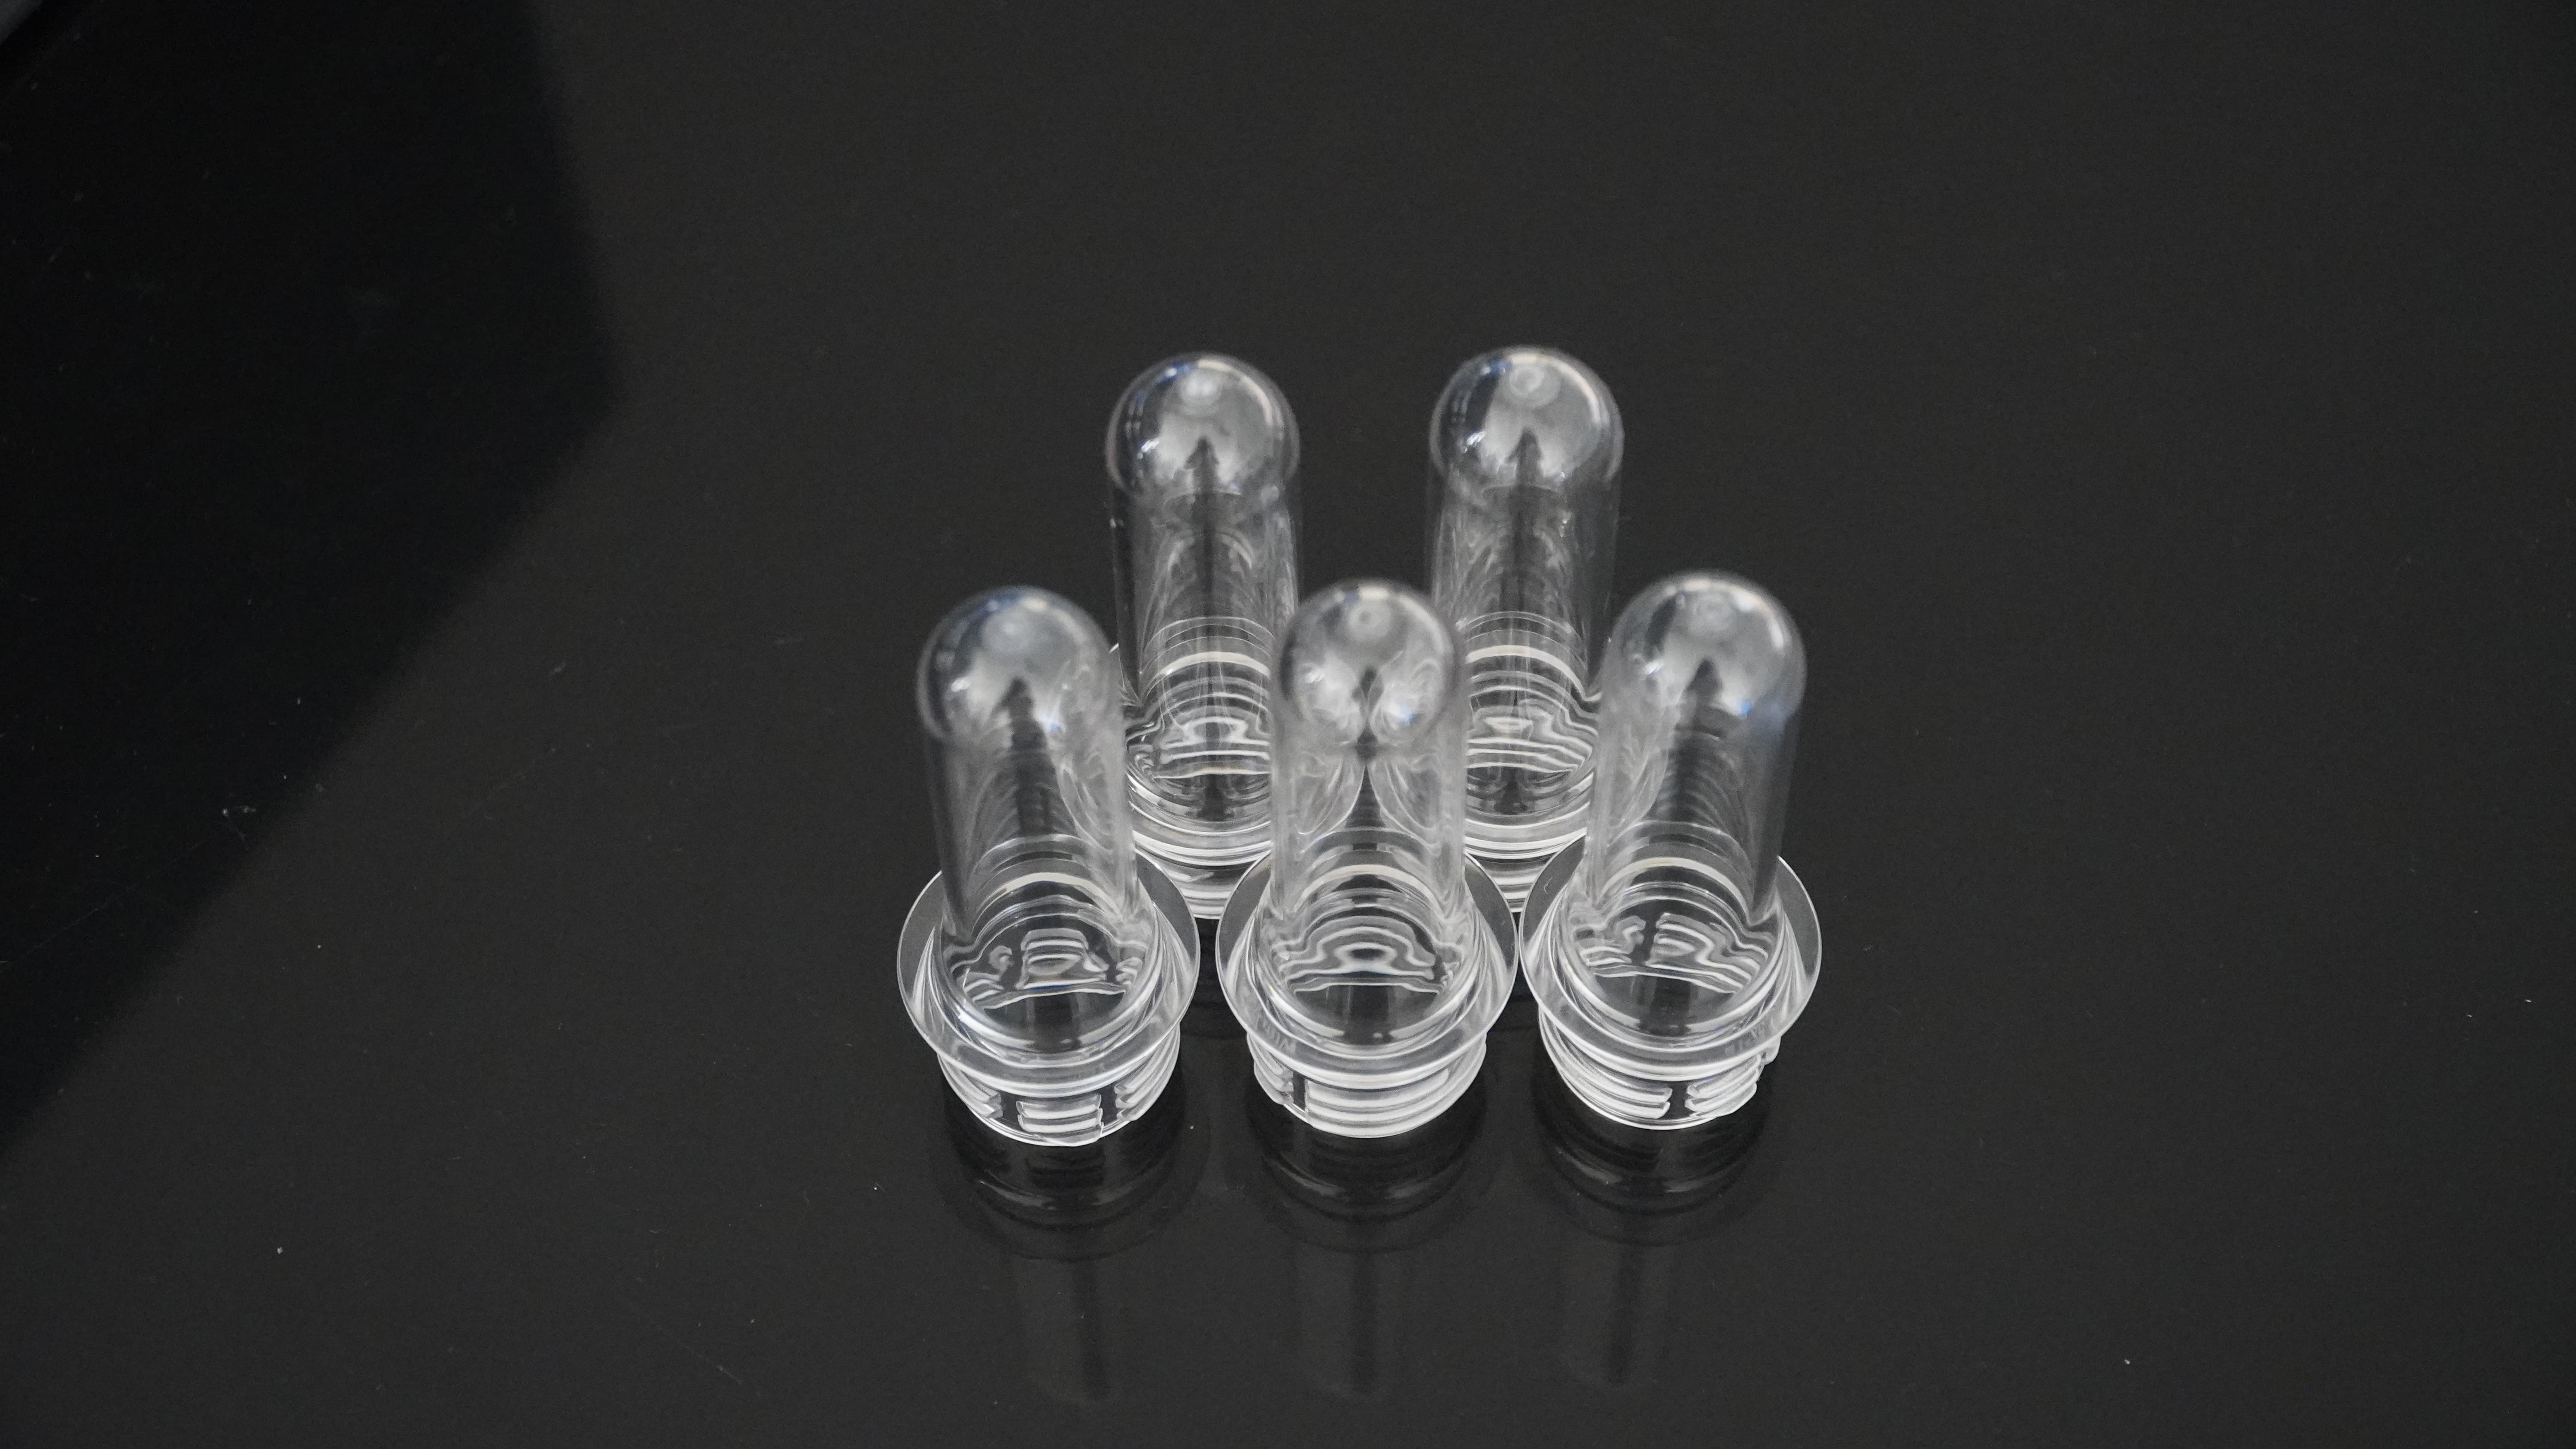
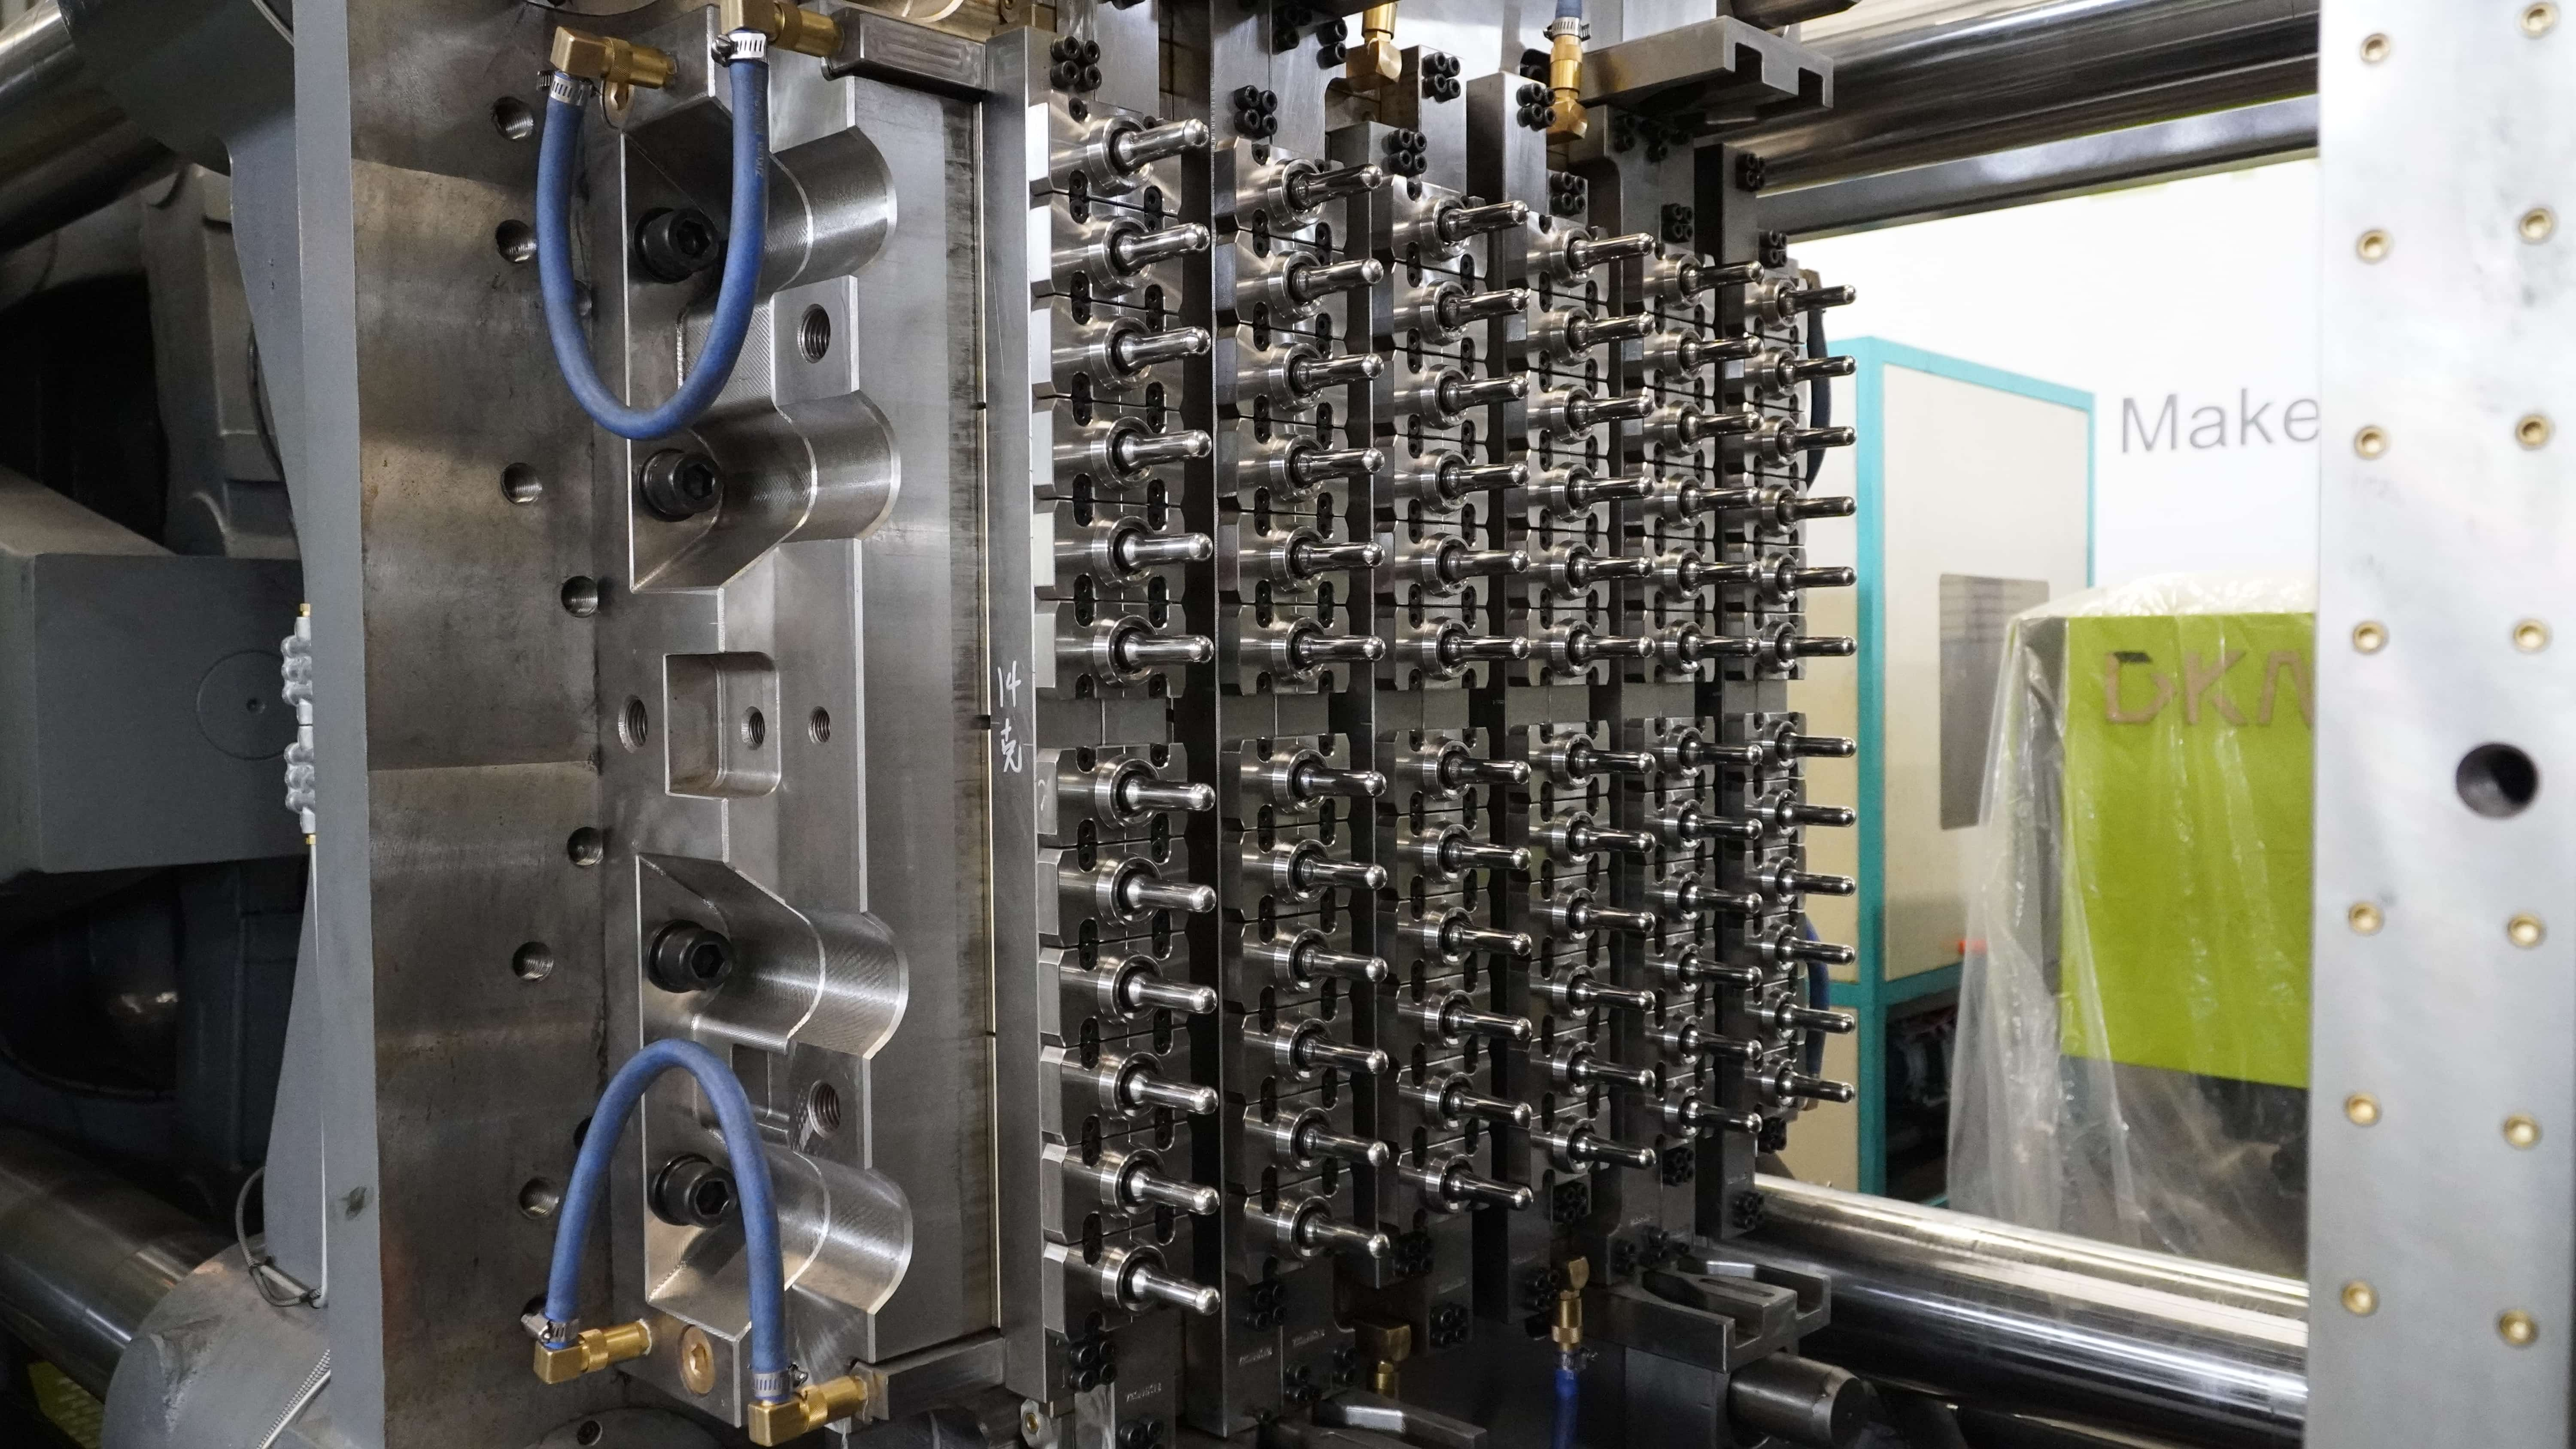
The PET Bottle Preform Mold, manufactured by Sino Mould and its subsidiary SINO-PK, supports cavity configurations from 8 up to 168. Key components use Swedish S136 steel (HRC45-48) with the mold base in DIN1.2311, holding tolerances down to 0.01mm for uniform wall thickness and concentricity, with precision capability reaching ±0.005mm. Standard neck finishes include PCO 1810, PCO 1881, and 28mm necks for preform weights typically between 12g and 30g — a range that covers many bottle categories used for liquid packaging. Over 200 sets of standard PET preform molds have been delivered worldwide, and the group has accumulated over 20 years of multi-cavity preform mold manufacturing expertise.
Delivery Speed Without Sacrificing Standards
One of the most frequently cited pain points for bottle producers is equipment lead time. DKM's standard 48/72-cavity production lines, built around standard 28/38mm neck finishes, move from order confirmation to qualified shipment in 14 days. Standard PET preform molds alone (48/72 cavity) can be delivered in as little as 7 days depending on configuration, while custom preform molds and lines — including special neck finishes, unique bottle designs, or mixed-cavity configurations — are completed in 5 to 7 weeks. This is supported by a secured supply chain with strategic inventory of critical components and safety stock maintained for the 350T, 450T, 550T, and 650T PET III models, allowing faster response when a customer needs equipment on a compressed timeline.
Automation at the Cooling and Pick Stage
A preform's weight class determines how it should be cooled after ejection. The Out-Mold Cooling & Pick Robot system cools preforms under 16g directly on the robot gripper during part removal, while preforms over 16g are combined with multi-station cooling units — an approach that avoids extending the mold cycle time just to accommodate a heavier preform. Dual-station and three-station external cooling robot configurations are matched specifically to the 72-cavity and 48-cavity line setups described above, and a take-out robot is integrated into the 144-cavity configuration.
Quality Verification Before Shipment
Every PET Preform Production Line undergoes a pre-factory acceptance test under simulated production conditions before shipment, reducing the risk of start-up delays once equipment reaches the customer's facility. This is paired with a 3-year warranty for PET preform molds, which includes free spare parts during the warranty period — a meaningful consideration for any producer evaluating total cost of ownership rather than purchase price alone.
Delivery Track Record
Documented production examples include a 72-cavity PET preform production line with an out-mold cooling system producing a 13.5g, 28mm neck preform at a 12-second cycle, and 48/72/96-cavity standard lines available with 14-day delivery for standard 28/38mm neck finishes. In one instance, 48 or 72-cavity preform mold delivery was completed within 3 weeks of order confirmation, with full line delivery within 4 weeks, for standard 28/38mm necks. Two 144-cavity PET preform production lines are currently operating in Iraq and Iran under normal production conditions, with customer acceptance test reports confirming satisfactory performance.
What This Means for Oil Bottle Preform Buyers
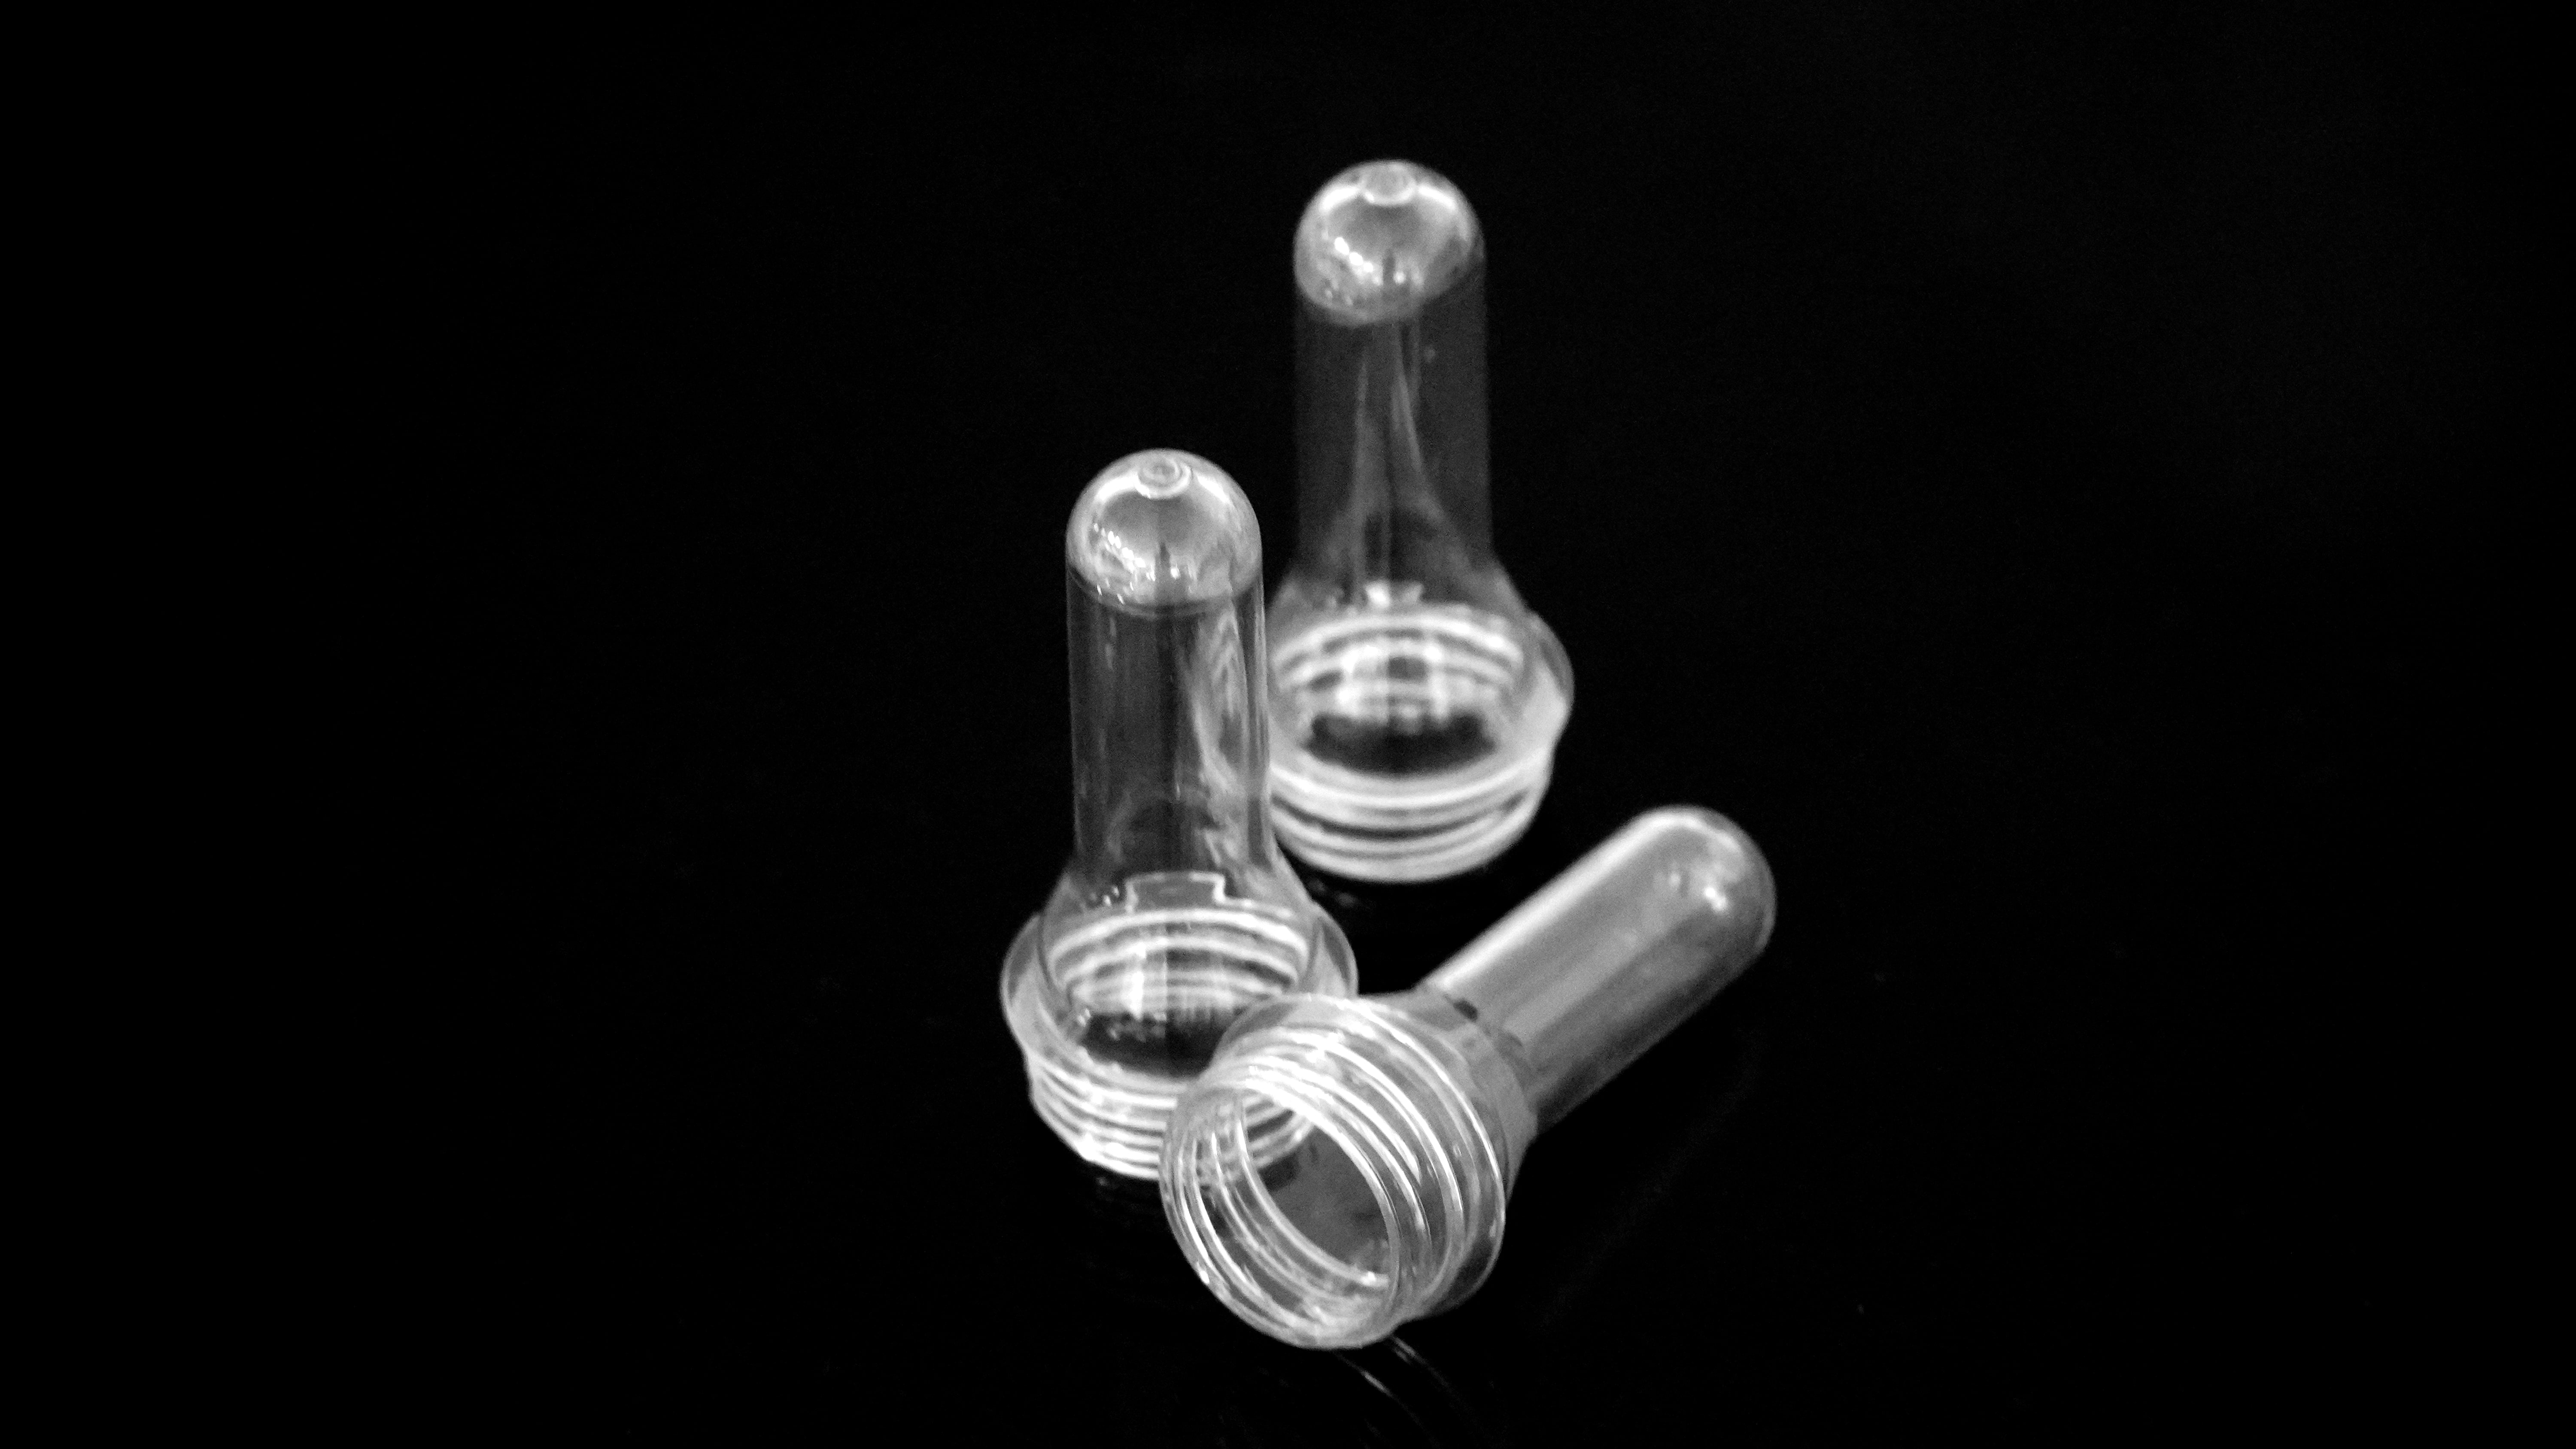
For companies evaluating a preform line for oil bottle production, the relevant engineering questions are the same as those governing any PET bottle preform application: cavity count versus required output, neck finish standard, preform weight range, and acceptable lead time. DKM Machinery and Sino Mould address these questions through standardized, pre-commissioned configurations supported under their Injection Moulding Technical Solutions framework — sometimes referenced as MoldingIT within the group's broader technical solutions branding — covering machine selection from 90T to 4000T, dedicated mold design, process commissioning, mass production guidance, on-site training, and professional engineering response within 24 hours. This combination of mold precision, machine repeatability, automation integration, and documented delivery timelines gives bottle producers a structured basis for comparing preform line options against their own production and lead-time requirements.
https://dkm.com/dfs-low-inertia-high-speed-machine/
DKM Machinery

+ There are no comments
Add yours